
A pump begins to shake more than usual. A fan develops a low, steady hum. Production staff notice vibration at the motor housing and assume the bearings are failing.
That conclusion is sometimes correct. Bearings are common wear components, and damaged ones can create heat, noise, looseness, and serious secondary damage. But replacing bearings because a machine vibrates can also be an expensive misdiagnosis.
Many rotating-machine problems originate in rotor unbalance: an uneven distribution of mass around the axis of rotation. The correction may be a carefully placed balance weight, not a bearing change.
The distinction matters because balance correction, bearing replacement, alignment, and structural repair solve different faults. Good maintenance begins by identifying the vibration mechanism rather than treating the nearest visible component.
🔄 Start with the Difference Between Unbalance and Bearing Failure
Unbalance occurs when a rotor’s mass center does not lie exactly on its rotational centerline. As the shaft turns, that offset mass produces a rotating centrifugal force that repeatedly pushes on the shaft, bearings, and machine structure.
Bearing failure is different. A rolling-element bearing may have raceway damage, rolling-element defects, inadequate lubrication, contamination, incorrect internal clearance, or mounting damage. These conditions create characteristic vibration, friction, and sometimes temperature changes.
A balanced rotor can still destroy poor bearings, and new bearings can still be overloaded by an unbalanced rotor. The practical question is not which fault is more familiar; it is which fault best explains the measured symptoms.
🎯 Why a Small Mass Error Can Create a Large Force
The force from unbalance rises strongly with speed. In simplified form, unbalance force depends on the unbalanced mass, its distance from the shaft centerline, and the square of rotational speed.
That squared speed relationship explains why a fan that seems acceptable at low speed may vibrate severely near full speed. Doubling rotational speed does not merely double the unbalance force; under otherwise similar conditions, it increases it by roughly four times.
Imagine a small washer stuck near the rim of a bicycle wheel. At walking speed it is barely noticeable. At high speed, its repeated outward pull becomes much more significant.
📍 Recognize the Classic 1× Running-Speed Pattern
The most familiar signature of unbalance is vibration at 1× running speed, meaning one vibration cycle for each shaft revolution. A machine operating at 1,800 rpm, for example, has a running frequency of 30 Hz.
In a vibration spectrum, unbalance often appears as a prominent peak at that frequency. The vibration is commonly strongest in radial directions—horizontal or vertical—because the rotating force acts perpendicular to the shaft axis.
A 1× peak alone does not prove unbalance. Misalignment, bent shafts, eccentric components, looseness, resonance, and some fluid forces can also produce substantial running-speed vibration. Phase readings and operating observations are needed to narrow the diagnosis.
📈 Use Amplitude, Phase, and Direction Together
Reliable diagnosis rarely comes from one overall vibration number. Analysts compare amplitude, frequency content, vibration direction, and phase, which describes the timing of one signal relative to a reference mark on the rotating shaft.
For a simple rigid rotor with dominant unbalance, radial vibration at the two bearing locations often has a reasonably stable phase relationship. The response should also repeat consistently at the same operating speed and load condition.
If readings change unpredictably, phase wanders, or axial vibration dominates, the problem may not be simple unbalance. That does not make balancing useless, but it means adding a weight before further investigation can obscure the real fault.
🧭 Know What Bearing Damage Usually Looks Like
Rolling-element bearing defects often produce vibration frequencies related to the bearing geometry: cage frequency, ball or roller spin frequency, and frequencies associated with the inner and outer races. These are not usually exactly equal to shaft running speed.
Early bearing damage may be easier to detect with high-frequency acceleration measurements, enveloping or demodulation methods, ultrasound, lubricant inspection, or temperature trends than with a basic overall vibration reading.
Defect frequencies can have sidebands and may be masked by machine noise, variable speed, or poor sensor placement. Bearing diagnosis is therefore probabilistic and condition-based, not a matter of matching one peak to a chart without context.
👂 Listen for Noise, but Do Not Diagnose by Sound Alone
A smooth, speed-related hum can accompany unbalance, particularly in fans and blowers. A rougher, crackling, growling, or intermittent sound may suggest damaged rolling surfaces, poor lubrication, or contamination.
However, machine sound travels through guards, pipework, foundations, and enclosures. A noisy coupling or airflow disturbance can make a healthy bearing sound suspect, while a defective bearing can be almost inaudible in a loud process area.
Use hearing as a screening clue. Confirm it with measurements, inspection history, and the operating pattern of the machine.
🌡️ Treat Temperature as Supporting Evidence
Friction-related bearing problems can raise bearing housing temperature, especially if lubrication is inadequate or a bearing is badly damaged. Temperature that continues to rise at a steady load deserves attention.
Unbalance can also raise temperature indirectly. The added dynamic load increases bearing load and can flex supports, but a modest balance issue does not automatically produce a hot bearing.
Compare like with like: the same location, load, ambient condition, and instrument method. An isolated temperature reading is much less useful than a repeatable trend.
🛢️ Check Lubrication Before Condemning the Bearing
Incorrect lubricant type, too little grease, too much grease, contaminated oil, water ingress, and blocked lubricant paths can all cause bearing distress. Over-greasing is especially easy to overlook; excess grease can churn and generate heat.
Before scheduling replacement, review lubrication practices and inspect available evidence such as grease condition, oil appearance, filter debris, or automatic lubricator settings. Correcting lubrication will not repair a spalled raceway, but it may explain a temperature or noise problem without a bearing change.
Lubrication evidence should never be used to dismiss severe vibration. It is one part of a fault picture.
🧱 Rule Out Mechanical Looseness
Loose hold-down bolts, cracked feet, soft foot, worn fits, loose bearing housings, and degraded foundations can amplify vibration. The machine may look unbalanced because its structure is responding dramatically to a relatively small rotating force.
Mechanical looseness frequently produces harmonics of running speed—2×, 3×, and higher multiples—and may create impact-like waveforms. But the exact spectrum depends on the machine and severity.
Check fasteners, base condition, shims, grout, and bearing housing fits before balancing. A balance correction on a loose machine can be misleading and may not remain valid after the structure is repaired.
📐 Separate Shaft Misalignment from Unbalance
Misalignment occurs when coupled shafts are not collinear during operation. Angular and offset misalignment impose cyclic forces through the coupling and can damage couplings, seals, and bearings.
Misalignment often creates elevated axial vibration and may show strong 1× and 2× components. It can coexist with unbalance, so replacing bearings or balancing a rotor alone may leave the underlying load path unchanged.
Measure alignment with appropriate tools and account for thermal movement. A motor and pump aligned when cold may shift as their casings reach operating temperature.
🌀 Consider Eccentricity and Bent Shafts
Eccentricity means a rotating component’s geometric center differs from its intended centerline. A pulley, sheave, gear, or rotor may be mounted off-center, or a shaft may be bent.
These faults can produce strong 1× vibration similar to unbalance. The difference is practical: adding correction weight may reduce the measured response at one location while leaving a geometric or shaft problem in place.
Runout checks, dial indicators, and inspection during shutdown can distinguish a bent shaft or eccentric fit from a purely mass-related imbalance.
🏗️ Watch for Resonance Near Certain Speeds
Resonance occurs when running speed or one of its excitation frequencies approaches a natural frequency of the rotor, support structure, piping, or guard. At resonance, even a small force can produce a large vibration response.
A key clue is a sharp amplitude increase over a narrow speed range during run-up or coast-down. The phase often changes rapidly as the machine passes through the resonant region.
Balancing may reduce excitation and help, but it may not be the complete solution. Stiffening supports, changing operating speed, modifying rotor stiffness, or addressing structural connections can be necessary.
💨 Account for Process and Aerodynamic Forces
Fans, pumps, compressors, and mixers are not isolated rotors. Flow instability, cavitation, recirculation, impeller damage, blade passing effects, pressure pulsation, and changing product properties can drive vibration.
For example, a pump that vibrates only at low flow may be operating away from its preferred hydraulic range. Rebalancing the impeller will not correct a system condition that produces internal flow separation or cavitation.
Compare vibration with process variables such as flow, pressure, valve position, fluid level, and product density. A fault tied closely to process condition requires a process-aware diagnosis.
⚖️ Understand Single-Plane and Two-Plane Balancing
A narrow, rigid rotor can often be corrected in one plane. A weight is added or removed at a calculated angular position to bring the rotor’s mass center closer to the rotation axis.
Longer rotors may require correction in two planes. This addresses both static unbalance and couple unbalance, where unequal mass distribution causes a rocking tendency even if the overall center of mass appears centered.
Two-plane balancing is common for rotors such as long fans, armatures, and multi-stage assemblies. The appropriate method depends on rotor geometry, operating speed, support arrangement, and flexibility.
🧪 Decide Between Shop Balancing and Field Balancing
Shop balancing is performed on a balancing machine, typically with the rotor removed. It is useful after fabrication, repair, impeller replacement, coating, machining, or major overhaul.
Field balancing is performed in the installed machine using vibration and phase measurements. It incorporates the actual assembled condition: shaft, coupling, supports, and sometimes the influence of attached components.
Neither method is universally better. Shop balancing is often preferred for removed components and controlled correction, while field balancing is valuable when removal is impractical or when installed-system response is the central concern.
🧰 When Rebalancing Is Usually the Better First Action
Rebalancing becomes a strong candidate when evidence points to a stable mass-distribution problem and the bearings show no convincing signs of distress. Typical situations include:
- Vibration is dominated by a repeatable 1× running-speed component.
- Radial vibration is more prominent than axial vibration.
- Phase measurements are stable and support an unbalance interpretation.
- The issue began after impeller erosion, buildup, blade repair, material loss, or rotor modification.
- Bearings have normal or stable temperature, acceptable lubrication condition, and no clear defect-frequency evidence.
- The vibration changes predictably with speed rather than appearing only under a particular process upset.
These are decision clues, not a substitute for machine-specific acceptance criteria or competent analysis.
🛑 When Bearing Replacement Should Take Priority
Replace or repair bearings when inspection or condition monitoring indicates actual bearing damage, or when continued operation creates an unacceptable risk. Rebalancing cannot restore a pitted raceway, fractured cage, seized rolling element, or severely damaged fit.
Priority signs can include increasing high-frequency bearing-defect indicators, abnormal heat linked to the bearing, metallic debris in lubricant, roughness during manual rotation when safely isolated, or visible damage discovered during inspection.
If the bearing is near functional failure, deal with it first. Then assess whether rotor balance, alignment, installation practice, or operating load contributed to the damage.
🔍 Inspect the Rotor for Material Change
Rotor balance changes when mass is added, removed, moved, or redistributed. Dust accumulation on one side of a fan, product buildup on a mixer blade, corrosion loss, broken impeller vanes, and uneven wear are all common causes.
A clean fan may vibrate little, while the same fan gradually becomes unbalanced as sticky material accumulates. In that situation, a balance job without correcting the contamination source may provide only short-term relief.
Inspect for loose balance weights, cracked welds, missing hardware, damaged blades, and deposits. The physical cause of the imbalance should be removed or controlled before final correction.
🧹 Do Not Balance Over Dirt, Damage, or a Loose Weight
A common mistake is attaching a trial or permanent weight to compensate for an unknown condition. If the real problem is a deposit that later falls off, the added weight becomes the new imbalance.
Likewise, a loose existing balance weight can mimic an evolving rotor issue. Repair the attachment method and confirm the component is structurally sound before making corrections.
Balance correction should be durable, documented, and appropriate for the rotor. Temporary test weights must be secured and managed under a controlled procedure.
📊 Build a Baseline Rather Than Chasing One Reading
A useful condition-monitoring program records vibration by location and direction, rotational speed, load, temperature, process state, and relevant maintenance events. Trend data reveal whether a change is gradual, sudden, load-sensitive, or speed-sensitive.
A machine with historically low 1× vibration that rises after an impeller repair deserves a different investigation from a machine that has always operated near the same level. Its own baseline is often more informative than a single isolated number.
Alarm limits must be selected for the machine, its service, and the organization’s risk tolerance. Generic limits can be useful screening tools, but they do not replace engineering judgment.
🧑🔧 Follow a Safe Field-Balancing Workflow
Field balancing involves rotating machinery, temporary weights, measurement equipment, and sometimes exposed coupling areas. It should be performed only by trained personnel using a documented method and the site’s safety controls.
- Confirm operating condition, speed, and sensor/reference setup.
- Inspect for looseness, damage, rubs, buildup, and obvious alignment concerns.
- Collect baseline vibration and phase data at repeatable conditions.
- Install a securely retained trial weight in a planned correction plane.
- Measure the response change and calculate the correction weight and angle.
- Install the permanent correction, rerun the machine, and verify the result.
- Record final readings, weight details, and any residual concerns.
Never improvise weight attachment on a high-speed rotor. A released weight is a serious projectile hazard.
📏 Know the Limits of Acceptable Balance
“Perfectly balanced” is not a realistic maintenance target. Every rotor retains some residual unbalance, and the acceptable amount depends on rotor mass, operating speed, geometry, service severity, and machine sensitivity.
Precision machinery and high-speed rotors generally require tighter control than low-speed, rugged equipment. But overly aggressive balancing can also consume resources without meaningfully improving reliability if the remaining vibration comes from structure, process, or another fault.
The objective is a suitable residual vibration and unbalance condition for the machine’s duty—not the lowest possible instrument reading in isolation.
🔧 Replace Bearings Correctly When They Are Needed
When bearing replacement is justified, the job should also address the reason the bearing failed. Otherwise, the machine may return to service with new components exposed to the same overload or installation damage.
Review shaft and housing fits, cleanliness, mounting force path, preload or clearance requirements, lubrication, sealing, alignment, and rotor condition. Never transmit installation force through rolling elements when mounting a bearing.
After replacement, collect new baseline data. A new bearing may lower high-frequency defect activity while a persistent 1× problem reveals that unbalance was present all along.
🧩 Consider How Faults Interact
Real machinery often has more than one fault. Unbalance increases alternating bearing load; misalignment adds cyclic forces; poor lubrication reduces the bearing’s ability to tolerate them. Over time, one problem can create evidence of another.
This interaction explains why an either-or question can be misleading. A damaged bearing may need replacement, while the root cause still requires balancing, alignment correction, or process changes.
Use a sequence: stabilize immediate risk, repair confirmed damage, correct contributors, and verify under normal operation.
🏭 Example: The Dust-Loaded Exhaust Fan
Consider a hypothetical belt-driven exhaust fan that develops increasing vibration over several weeks. The vibration is primarily radial at fan running speed, and the trend tracks dust buildup on the blades.
The bearings are not unusually hot, lubrication is satisfactory, and detailed measurements do not show a clear bearing-defect pattern. Cleaning the rotor, inspecting blade condition, and field balancing after cleaning are sensible actions.
Replacing bearings first may temporarily reduce noise if new bearings are quieter, but it would leave the rotating-force source in place. The corrected fan should still be monitored because prior unbalance may have shortened bearing life.
⚙️ Example: The Motor with a Genuine Bearing Fault
Now consider a hypothetical electric motor with rising high-frequency vibration at the drive-end bearing, increasing localized temperature, and lubricant evidence consistent with contamination. Its overall 1× vibration may also be elevated because the damaged bearing has increased clearance.
In this case, balance correction is not the first remedy. The bearing condition needs inspection and likely replacement, with attention to contamination control and mounting practice.
After repair, vibration testing can determine whether remaining 1× response points to rotor unbalance, soft foot, alignment, or another condition that was masked by the bearing fault.
🚫 Avoid the “New Parts Must Fix It” Assumption
Replacing bearings is tangible and often necessary, but it is not a universal vibration cure. New bearings can fail quickly if an unbalanced fan, misaligned coupling, resonance condition, or overloaded process remains uncorrected.
The reverse mistake is equally costly: continuing to balance a machine with damaged bearings because 1× vibration is visible. A balance correction may lower one symptom while a bearing defect continues to progress.
Maintenance quality improves when the repair is tied to a defensible fault mechanism rather than the most convenient available action.
📝 Ask These Questions Before Choosing the Repair
- What frequency components dominate, and do they repeat at the same operating condition?
- Is the response mostly radial, axial, or highly direction-dependent?
- What do phase measurements indicate?
- Did the problem follow cleaning, buildup, erosion, repair, impact, or a process change?
- Are bearing temperature, lubrication, and high-frequency indicators changing?
- Have alignment, soft foot, hold-down bolts, and structural integrity been checked?
- Does vibration rise at a particular speed or with a particular flow or load?
- What did the machine’s historical baseline look like?
Clear answers do not eliminate uncertainty, but they greatly reduce guesswork.
🧠 The Core Principle: Diagnose the Force Before Replacing the Part
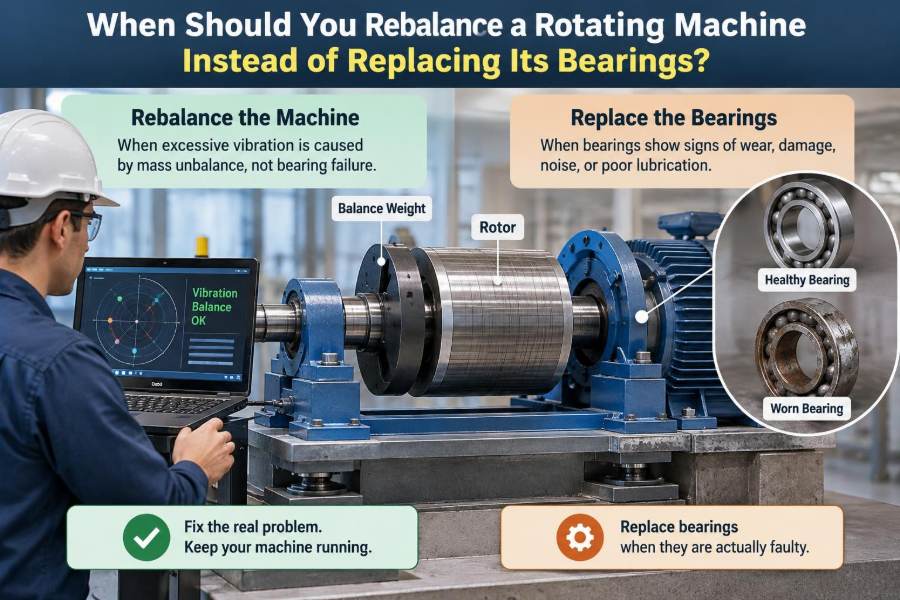
Rebalance a rotating machine when the evidence supports a stable rotor-mass problem: typically repeatable running-speed vibration, a coherent phase response, a credible source of mass change, and no strong indication that the bearings themselves are failing.
Replace bearings when their condition is demonstrably poor or when their continued service is unsafe. Then investigate why they deteriorated, because unbalance, misalignment, lubrication errors, and contamination often contribute to bearing damage.
The best decision is not “balance versus bearings” as a habit. It is a structured diagnosis of the forces, frequencies, operating conditions, and physical evidence affecting the machine.
Rebalance the rotor when unbalance is the cause; replace the bearings when bearing damage is the cause—and address both when the evidence shows they are connected. ⚙️📈🛠️