
A door hinge begins to squeak. A bicycle chain feels rough after a wet ride. A production line loses output because a bearing runs hot. These are familiar problems, but they arise from the same engineering challenge: two surfaces are moving against each other.
That challenge is rarely as simple as choosing a “slippery” material. Surface roughness, load, speed, temperature, contamination, chemistry, and lubricant supply can all determine whether a component operates smoothly or fails early.
The field that studies these interactions is tribology: the science and engineering of friction, wear, lubrication, and interacting surfaces in relative motion. Its discoveries have shaped engines, turbines, railways, artificial joints, computer drives, manufacturing tools, and countless everyday mechanisms.
Understanding the milestones in tribology does more than explain history. It gives engineers a practical way to diagnose contact problems, choose materials, and reduce energy loss without creating a new reliability problem elsewhere.
🔍 Tribology Begins at the Contact Interface
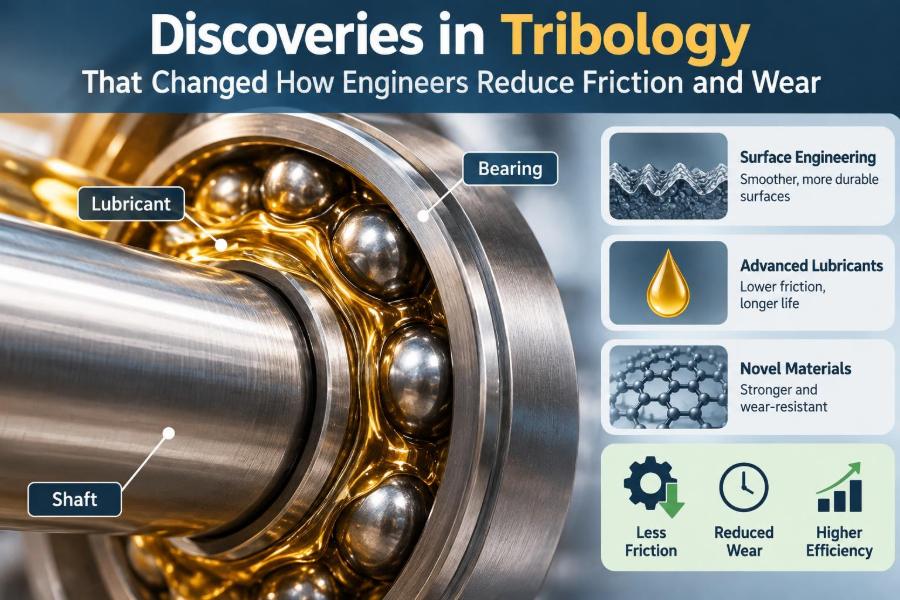
Tribology focuses on the interface between surfaces rather than treating a machine as a collection of isolated parts. A shaft and bearing, gear teeth, a cutting tool and workpiece, or a tire and road are all tribological systems.
At each interface, engineers ask four linked questions: What friction is produced? What wear mechanism is active? Is a lubricant or protective film present? How do load, motion, and environment change the answer?
📐 Amontons’ Laws Made Friction Measurable
Early experiments associated with Guillaume Amontons established a useful idealization: dry-friction force is approximately proportional to normal load and is often relatively insensitive to apparent contact area. This led to the familiar model F = μN, where μ is the coefficient of friction.
The model remains valuable for preliminary calculations, brakes, clamps, and basic force estimates. But it is not a complete description of real engineering contacts, especially when surfaces are lubricated, rough, elastic, hot, or chemically changing.
🧱 Real Contact Area Changed the Picture
A major insight was that nominal contact area is not the same as real contact area. Even polished solids touch first at microscopic high points called asperities.
Under load, those asperities deform. The true area carrying load can be far smaller than the visible contact patch, producing very high local pressures. This explains why friction, wear, and surface damage often begin in places that a simple drawing does not reveal.
🧲 Adhesion Explained Why Smooth Surfaces Can Stick
When clean asperities meet under pressure, atoms at the interface can form adhesive junctions. Sliding requires these junctions to shear or break, contributing to friction.
This discovery corrected the idea that friction is merely one rough surface “climbing over” another. Roughness matters, but adhesive interaction matters too. In vacuum or exceptionally clean environments, adhesion can become especially troublesome because ordinary atmospheric films are absent.
🛢️ Reynolds Built the Foundation of Hydrodynamic Lubrication
Osborne Reynolds showed that a moving surface can drag a viscous lubricant into a converging gap and generate pressure within the fluid. That pressure can support the applied load and separate the solid surfaces.
This is hydrodynamic lubrication. A journal bearing is a classic example: as the shaft rotates, it rides on an oil film rather than directly on the bearing shell once operating conditions are established.
🌊 The Wedge Film Is a Designed Load-Carrying Element
The oil film in a hydrodynamic bearing is not simply a bath of lubricant. Its ability to carry load depends on a wedge-shaped clearance, relative speed, fluid viscosity, and a sufficient supply of oil.
A useful intuition is aquaplaning: motion can generate a pressure-bearing fluid layer. The engineering difference is that bearings use controlled geometry and lubricant properties to create that effect predictably.
📉 The Stribeck Curve Connected Regimes of Lubrication
The Stribeck curve describes how friction changes as the conditions supporting a lubricant film improve. It connects low-speed, heavily loaded contacts with high-speed contacts where a thicker fluid film can separate surfaces.
| Lubrication regime | Surface relationship | Typical concern |
|---|---|---|
| Boundary | Asperities carry much of the load | Wear and film chemistry |
| Mixed | Fluid film and asperities share load | Transition damage and friction |
| Hydrodynamic or full-film | Fluid separates surfaces | Viscous drag and temperature |
The curve is a guide, not a universal component law. Real contacts may experience several regimes during every start, stop, load change, or temperature shift.
🚦 Boundary Lubrication Solved the Start-Stop Problem
Many machine elements cannot remain fully separated by a fluid film. Engine components at start-up, slow oscillating joints, and heavily loaded gear contacts may operate in boundary lubrication.
Here, molecularly thin films and surface-reactive additives reduce shear and protect asperities. The discovery mattered because adding more bulk oil does not automatically prevent contact when speed is low or the fluid film is too thin.
🧪 Additive Chemistry Made Lubricants Active Materials
Lubricants evolved from passive fluids into carefully formulated materials. Antiwear additives, extreme-pressure additives, antioxidants, corrosion inhibitors, detergents, dispersants, and friction modifiers each address different risks.
Some additives react at the surface under specific conditions to form sacrificial protective films. Their performance depends on temperature, load, material pairing, and lubricant chemistry; a useful additive in one system can be unsuitable in another.
🧬 Tribofilms Protect by Being Sacrificial
A tribofilm is a thin layer created or maintained at a rubbing interface by lubricant chemistry, transferred material, or surface reaction. It may shear more readily than the base metal and limit direct asperity welding.
That protection is not permanent. Film formation can require time and appropriate conditions, while abrasive particles, excessive heat, or incompatible additives can disrupt it. Engineers therefore assess the whole lubricant-system combination rather than an additive in isolation.
🪨 Abrasive Wear Revealed the Damage of Small Particles
Abrasive wear occurs when hard asperities or particles cut, plough, or fracture a softer surface. A dusty hydraulic system, contaminated gearbox, or machining operation with trapped debris can all develop this mechanism.
The practical discovery is straightforward but powerful: cleanliness is a design variable. Seals, breathers, filtration, clean assembly procedures, and controlled lubricant handling can preserve surfaces more effectively than repeatedly replacing damaged parts.
🔗 Adhesive Wear Explained Scuffing and Galling
Adhesive wear occurs when local junctions form between sliding surfaces and material transfers or tears away during motion. Severe forms include scuffing in heavily loaded sliding contacts and galling in threaded fasteners or stainless-steel components.
Material pairing, surface finish, load, speed, lubrication, and heat all influence the risk. Similar metals sliding under poor lubrication can be particularly prone to transfer because their junctions may shear within the bulk material rather than at a benign interface.
🔄 Fatigue Wear Exposed the Cost of Repeated Stress
Rolling bearings and gear teeth often fail through rolling-contact fatigue rather than simple rubbing wear. Repeated subsurface stresses can initiate cracks that eventually produce pits, spalls, or flaking.
This finding shifted attention toward contact stress, hardness gradients, inclusions, heat treatment, alignment, and lubricant-film thickness. A smooth, low-friction contact can still have inadequate fatigue life if its stress field is poorly managed.
⚗️ Tribocorrosion Joined Chemistry to Mechanics
Tribocorrosion occurs when wear and corrosion reinforce each other. Sliding may remove a passive oxide layer, exposing fresh metal; the environment then attacks that metal before the protective layer can reform.
This matters in marine equipment, chemical processing, biomedical implants, and humid environments. A corrosion-resistant alloy is not automatically tribocorrosion-resistant, because mechanical removal changes the surface chemistry continuously.
🧊 Elastohydrodynamic Lubrication Explained Rolling Contacts
In concentrated contacts such as gears and rolling bearings, pressure can be extremely high. The surfaces elastically deform, while the lubricant’s viscosity rises strongly with pressure. This regime is called elastohydrodynamic lubrication, or EHL.
EHL theory explained how remarkably thin films can separate surfaces in loaded rolling contacts. It also clarified why lubricant viscosity, rolling speed, surface roughness, and temperature must be evaluated together.
⚙️ Gear Teeth Demonstrated Mixed Lubrication in Motion
Gear meshes are rarely simple. Conditions vary along the tooth profile as sliding direction and speed change, while loads fluctuate and oil may be thrown, sprayed, or channeled into the mesh.
Near the pitch point, rolling is dominant; away from it, sliding becomes more significant. Gear design therefore balances tooth geometry, surface finish, lubricant formulation, operating temperature, and alignment rather than relying on one friction coefficient.
🧭 Surface Texture Became an Engineered Feature
Machining marks, honing patterns, and deliberately created microtextures can influence lubricant retention, debris movement, contact pressure, and running-in behavior. Surface finish is therefore more than an aesthetic specification.
Texture is not universally beneficial. Grooves in the wrong direction, excessive roughness, or poorly controlled dimples can raise friction or concentrate stress. The useful question is whether the texture supports the intended lubrication regime and direction of motion.
🧱 Hard Coatings Expanded Material Choices
Hard coatings such as nitrides, carbides, and diamond-like carbon variants can improve resistance to wear, scuffing, or adhesive transfer in suitable applications. They allow a component’s surface behavior to differ substantially from its structural core.
Yet a hard coating is not a cure-all. Adhesion to the substrate, coating thickness, residual stress, counterface compatibility, lubricant additives, and edge geometry all affect reliability. A brittle or poorly supported coating can crack and create abrasive debris.
🌡️ Temperature Turned Friction into a Thermal Problem
Friction converts mechanical work into heat. At a microscopic junction, the local temperature can differ greatly from a measured bulk component temperature, especially during severe sliding.
Heat lowers lubricant viscosity, accelerates oxidation, changes material properties, and can destabilize protective films. Thermal management may require oil flow, cooling passages, lower sliding speed, different materials, or geometry that spreads the contact load.
💧 Water Contamination Changed Lubricant Life
Water in lubricants can promote corrosion, alter additive behavior, reduce film performance, and impair bearing fatigue life. It may enter through condensation, leaking coolers, poor storage, washing, or damaged seals.
Not every system needs the same moisture-control strategy. The correct approach depends on lubricant type, operating temperature, environmental exposure, and component sensitivity, but identifying the entry route is more useful than merely draining and refilling oil.
🧹 Filtration Became a Reliability Tool
Filter selection involves more than choosing the smallest pore rating. Engineers consider particle size distribution, flow rate, pressure drop, bypass behavior, contaminant type, and where debris is generated.
A filter that is too restrictive can starve a system or remain in bypass; one that is too coarse may allow damaging particles to circulate. Good practice treats filtration, seals, reservoir design, and maintenance cleanliness as one contamination-control system.
📡 Condition Monitoring Made Wear Visible Earlier
Oil analysis, vibration monitoring, temperature trends, acoustic methods, and debris inspection can reveal changing tribological conditions before a component stops functioning. No single signal diagnoses every failure mode.
For example, an increase in ferrous debris may suggest wear but does not by itself identify whether the source is a gear, bearing, or external contamination. Trending data against known operating changes is generally more informative than treating one result as a verdict.
🔬 Modern Instruments Opened the Nanoscale Interface
Surface profilometry, microscopy, spectroscopy, and nanoscale force measurements have made it possible to examine wear scars, reaction films, transfer layers, and roughness with far greater detail than early tribologists could access.
These tools support better models, but they do not remove engineering judgment. A tiny laboratory contact may not reproduce the heat flow, lubricant supply, vibration, or contamination found in a full-size machine.
🤖 Digital Models Need Physical Validation
Computational fluid dynamics, finite element analysis, multibody models, and data-driven monitoring can estimate film thickness, stress, temperature, and motion. Used well, they shorten design iterations and reveal interactions that are difficult to measure directly.
Inputs remain decisive. Incorrect viscosity data, unrealistic surface assumptions, or an omitted misalignment can create an impressively detailed but misleading prediction. Test evidence and inspection remain essential for validating a tribological model.
🚗 Electrification Creates New Tribology Questions
Electric drivetrains often operate with different speed ranges, thermal patterns, lubricant requirements, and electrical conditions than conventional powertrains. Bearings may also face electrical discharge damage if currents pass through contact interfaces.
The lesson is not that established lubrication theory has become obsolete. Rather, component designers must revisit material selection, insulation, lubricant compatibility, electrical grounding, and high-speed film behavior for the new duty cycle.
🦴 Biotribology Brought Friction Science into the Body
Natural joints demonstrate highly effective lubrication under complex loads, motion, and biological constraints. Artificial joints must manage contact stress, wear debris, lubrication by body fluids, material compatibility, and long service demands.
Biomedical tribology is a reminder that low friction alone is not the objective. Wear products and chemical interactions can matter as much as mechanical efficiency, so design decisions must be evaluated in their biological environment.
🧰 Design for the Actual Duty Cycle
A component that performs well at one speed and load may fail during frequent starts, shock loading, reversal, idling, or contamination exposure. Tribological design begins by describing the real duty cycle rather than a single nominal operating point.
- Map load, speed, temperature, motion type, and duration.
- Identify likely lubrication regimes during transients.
- Specify acceptable contamination and moisture limits for the component.
- Consider access for inspection, relubrication, and replacement.
This process often reveals that the most damaging condition is not normal operation, but start-up, misalignment, or a brief overload.
⚠️ Common Friction-Reduction Mistakes
One common mistake is selecting the lowest-viscosity lubricant solely to reduce churning losses. If the resulting film becomes too thin, wear and fatigue risk may increase. Another is specifying an extremely smooth surface without considering whether it can retain lubricant or complete running-in.
Engineers also sometimes treat friction reduction and wear reduction as identical goals. They often align, but not always: a coating may lower friction while introducing debris risk, or a more viscous oil may raise fluid drag while protecting a heavily loaded contact.
🧩 Match the Solution to the Failure Mechanism
Effective troubleshooting starts with evidence. A polished transfer scar, abrasive grooves, pitting, discoloration, and corrosion products point toward different mechanisms and therefore different remedies.
Before changing a material or lubricant, inspect the contact, review assembly history, verify alignment and loading, assess contamination, and confirm operating temperature. Replacing parts without identifying the mechanism can repeat the same failure under a new part number.
🌍 Efficiency and Durability Must Be Balanced
Reducing friction can lower energy consumption and heat generation, while extending component life can reduce material use and downtime. However, the lowest-friction option is not automatically the lowest-impact choice if it needs frequent replacement, difficult processing, or demanding maintenance.
A balanced tribological decision weighs energy loss, service life, lubricant life, manufacturing route, maintenance practice, and end-of-life considerations. The best answer depends on the application’s full operating context.
🧠 The Lasting Principle of Tribology
The central discovery of tribology is that surfaces in motion are dynamic systems. Their behavior emerges from mechanics, materials science, fluid behavior, heat transfer, chemistry, and the surrounding environment.
Engineers reduce friction and wear most reliably when they control the interface: maintain an appropriate separating film where possible, protect the surface where contact is unavoidable, manage heat and contamination, and verify performance under realistic conditions.
The most effective tribological solution is not a universally “slippery” material or lubricant, but a deliberately matched system of surfaces, film, load, motion, and environment. That systems view is why discoveries in tribology continue to shape dependable machines, from simple hinges to high-performance power systems. ⚙️🛢️🔬