
A pump begins to feel rough through the handrail. A fan that once ran quietly develops a low, steady hum. At first, the machine still delivers flow or air, so the change is easy to dismiss as normal industrial noise.
Then bearing temperatures begin to drift upward, fasteners need repeated tightening, or a flexible coupling shows unexpected wear. By that point, the original problem may be harder to isolate because vibration has started affecting several parts at once.
Shaft imbalance is a common source of rotating-machine vibration, but it is not the only one. Detecting it early means recognizing its characteristic pattern, measuring carefully, and resisting the urge to blame every vibration peak on imbalance.
The goal is not merely a smoother-running rotor. It is to reduce cyclic forces before they shorten bearing life, overload couplings, loosen supports, or mask another developing fault.
🔄 What Shaft Imbalance Actually Means
A shaft assembly is imbalanced when its mass is not distributed symmetrically around its intended axis of rotation. As the assembly spins, its center of mass travels in a circle rather than remaining on the rotational centerline.
That motion creates a rotating centrifugal force. The faster the rotor turns, the more strongly that force acts on bearings, housing structures, and connected components.
“Shaft imbalance” often describes the complete rotating assembly: shaft, impeller, fan wheel, pulley, coupling hub, key, sleeve, and attached hardware. A straight shaft can therefore be part of an imbalanced rotor.
🧲 Why the Force Grows So Quickly with Speed
The approximate unbalance force follows the relationship F = m × e × ω², where m is the unbalanced mass, e is its distance from the rotation axis, and ω is angular speed.
The squared speed term is the practical warning. A small mass error that seems harmless during slow turning can produce a large cyclic load at operating speed. Doubling rotational speed increases the force by roughly four times when all other conditions remain unchanged.
This is why high-speed motors, fans, centrifuges, grinders, and turbine-related equipment demand particularly careful balance control.
🎯 Static Imbalance: One Heavy Side
Static imbalance exists when the rotor has a heavy spot and will tend to rotate until that spot hangs at the bottom when supported on low-friction rollers. The correction can usually be made in one transverse plane.
Imagine a fan wheel with a small patch of buildup near one blade tip. Its mass center shifts away from the shaft centerline, creating a once-per-revolution rotating force.
Static imbalance is often easiest to understand and diagnose, but it is not the only type encountered in machines with appreciable axial length.
📐 Couple Imbalance: When Two Planes Disagree
Couple imbalance occurs when unbalance exists in two separate axial planes, with the heavy locations roughly opposite each other. The mass center may still lie on the centerline, so a simple static check can miss it.
As the rotor spins, the opposing unbalances produce a rocking moment. The shaft may respond differently at each bearing, often requiring correction in two planes.
Long rotors, wide fan wheels, armatures, and assemblies with components near both shaft ends are more likely to need two-plane balancing.
🧭 Dynamic Imbalance in Real Assemblies
In practice, many rotors have a combination of static and couple imbalance, commonly called dynamic imbalance. It cannot be fully corrected by adding or removing mass at only one axial location.
A field balancing procedure uses vibration amplitude and phase measurements to determine how much correction is needed and where to place it. The method may involve calculated trial weights or instrument-guided influence coefficients.
Dynamic balancing is not simply a more elaborate version of static balancing. It addresses both force and rocking effects across the rotor’s length.
👂 The Earliest Clues Operators Notice
Operators often identify a change before an instrument survey is scheduled. A persistent tonal hum, a new vibration felt on a guard, or an object that slowly migrates across a machine base can all justify investigation.
These observations are clues, not a diagnosis. Belt noise, resonance, misalignment, loose supports, and aerodynamic effects can produce similar impressions.
- A smooth but unusually strong vibration that rises with speed
- A repeating hum synchronized with rotation
- New rattling of guards, piping, or cable trays
- Fastener loosening after previously stable operation
- Increased vibration following cleaning, repair, or product buildup
Recording when the behavior began is especially valuable. A change immediately after an impeller replacement suggests a different starting point than a gradual rise during months of service.
📊 The Classic 1× Running-Speed Signature
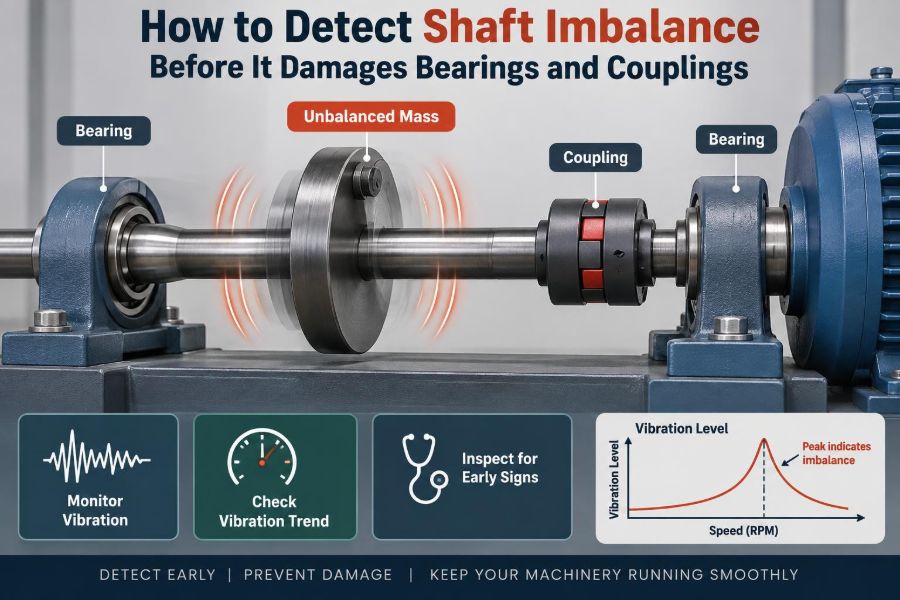
The most familiar vibration signature of imbalance is a dominant peak at one times running speed, usually written as 1×. A machine running at 1,800 revolutions per minute, for example, has a 1× frequency of 30 Hz.
On a vibration spectrum, imbalance often appears as a comparatively clean 1× component, particularly in the radial direction. Phase readings tend to be reasonably stable when measurements are repeated under similar conditions.
That pattern is useful, but not conclusive. Eccentricity, bent shafts, misalignment, looseness, and resonance can also create significant 1× vibration. A spectrum identifies a problem pattern; it does not replace mechanical judgment.
📏 Measure in the Right Directions
Vibration should normally be assessed in horizontal, vertical, and axial directions at relevant bearing housings. Radial readings—horizontal and vertical—are often most informative for imbalance because the rotating force acts perpendicular to the shaft axis.
Axial vibration should not be ignored. Strong axial response may point more strongly toward angular misalignment, thrust issues, or a structural path that is amplifying motion.
Measure at consistent locations with a properly mounted sensor. A loose magnetic base, hand-held probe, or changing sensor orientation can create misleading comparisons.
🕒 Use Phase to Separate Look-Alike Faults
Phase describes the timing of a vibration signal relative to a once-per-revolution reference, such as a reflective tape mark detected by an optical tachometer. It adds information that amplitude alone cannot provide.
For a stable imbalance condition, the phase at a given location often remains repeatable from one measurement to the next. During field balancing, phase indicates where the vibration vector lies and helps calculate a correction.
Phase relationships across bearings can also reveal rotor motion. Interpretation depends on machine configuration, support stiffness, sensor direction, and operating speed, so phase should be evaluated as part of a full measurement set rather than by a single rule.
🧾 Establish a Useful Baseline
The best time to learn a machine’s normal vibration pattern is when it is known to be mechanically sound. A baseline should include operating speed, load, process condition, measurement locations, sensor orientation, overall vibration, and spectrum data where available.
Without a baseline, technicians must compare the machine against general expectations or similar units. That can still be useful, but it is less sensitive to small changes unique to that installation.
Trend data matters because imbalance from deposits or erosion often develops gradually. A consistent upward movement at 1× can be more meaningful than one isolated high reading.
🧪 Compare Readings Across Operating Conditions
True mass imbalance generally becomes more evident as speed rises because its force increases with speed squared. If a variable-speed drive permits controlled testing, a speed sweep can be revealing.
Keep process conditions as steady as practical. A pump may behave differently with changing flow, and a fan can experience aerodynamic effects as dampers move.
Look for the overall pattern: does the 1× component rise smoothly with speed, or does it spike sharply near one narrow speed range? A sharp spike may indicate that a resonance is amplifying even a modest unbalance force.
🌉 Resonance Can Make Minor Imbalance Look Severe
Every mechanical structure has natural frequencies. When running speed or a harmonic approaches one of them, vibration can be amplified; this condition is called resonance.
A rotor with small residual imbalance may therefore vibrate strongly at a particular speed but acceptably above or below it. Balancing may reduce the forcing input, yet it may not fully solve a machine whose base, pedestal, guard, or piping is structurally resonant.
A coast-down or run-up test, performed only under an approved safe procedure, can help identify a narrow resonant zone. Structural corrections may include stiffening, changing support conditions, or avoiding a problematic continuous operating speed.
🧱 Inspect the Machine Before Balancing It
Field balancing a machine with loose feet, cracked welds, degraded grout, or an unstable base can produce poor results. The balance calculation may compensate for structural movement rather than rotor mass distribution.
Begin with a shutdown inspection when safe and appropriate. Check mounting bolts, baseplate condition, hold-down hardware, guards, pipe supports, and obvious evidence of rubbing.
Balance a mechanically sound machine. Correcting a rotor before addressing looseness often wastes time and can hide the actual fault.
🦶 Eliminate Soft Foot at the Motor
Soft foot occurs when one or more machine feet do not sit flat on the base. Tightening the hold-down bolts then distorts the machine frame, changing shaft alignment and sometimes the vibration response.
Check for soft foot before final alignment and before concluding that a motor-side 1× response is caused by imbalance. Correct it through clean contact surfaces and properly fitted shims, not by stacking random thin pieces.
The precise acceptance approach depends on the machine, coupling, and maintenance procedure. The essential point is that all feet must be supported consistently before measurements are trusted.
🔗 Distinguish Imbalance from Shaft Misalignment
Misalignment occurs when coupled shaft centerlines or angles are not properly matched. It can create radial and axial forces, coupling stress, heat, and vibration components at 1× and sometimes 2× running speed.
Unlike simple imbalance, misalignment frequently produces meaningful axial vibration and can affect both connected machines near the coupling. Flexible couplings tolerate limited misalignment; they do not remove the need for accurate alignment.
There is overlap between fault signatures, especially in real machines with multiple defects. Verify alignment after correcting soft foot and under conditions that account for expected thermal growth.
📎 Check Coupling Details and Assembly Errors
A coupling can contribute to rotating unbalance if one hub is damaged, a bolt set is incomplete, hardware is mixed, or a key projects improperly. A coupling guard should never be removed while the machine is operating, but coupling condition can be inspected during a controlled shutdown.
After maintenance, confirm that bolts, locking elements, keys, spacers, and hubs match the manufacturer’s assembly requirements. A missing balance feature or an incorrectly installed component can alter the rotor’s mass distribution.
Do not add arbitrary weight to a coupling to “cancel vibration.” Correction locations and methods must suit the component’s design and containment capability.
🪛 Examine the Rotor for Deposits and Damage
Many imbalance problems are service-induced rather than manufacturing defects. Material buildup on one fan blade, scale inside a pump impeller, uneven coating, corrosion loss, or a broken blade tip changes the mass distribution.
Inspect for asymmetry. On a fan, compare blade condition, attached debris, and erosion patterns. On a pump, inspect impeller passages and wear only after isolation, lockout, drainage, and other applicable safety steps.
Cleaning can solve an imbalance caused by deposits, but aggressive cleaning can also remove material unevenly. The post-cleaning condition should be checked, particularly on high-speed equipment.
🌀 Consider Bent Shafts and Rotor Eccentricity
A bent shaft or eccentric mounted component can also generate strong 1× vibration. These defects differ from simple mass imbalance because the shaft’s geometric centerline itself may orbit as it rotates.
Runout measurements with an appropriate indicator during shutdown can help identify geometric issues. Measurements must be interpreted carefully because surface damage, journal condition, and mounting reference affect the result.
If runout is excessive, adding balance weights may reduce vibration at one condition while leaving the underlying geometric problem in place.
⚙️ Do Not Forget Belts, Pulleys, and Gears
In belt-driven machines, pulley imbalance may be only one contributor. Belt tension, belt wear, pulley eccentricity, and sheave alignment can all alter the vibration pattern.
Gear-driven systems introduce gear-mesh frequencies and sidebands that may obscure a simple 1× assessment. A damaged gear or incorrect backlash should not be treated as a balance problem merely because vibration is present.
Map each relevant rotational speed, including motor, driven shaft, intermediate shaft, and fan or pump shaft. This prevents a peak from being assigned to the wrong component.
🌡️ Watch Bearing Temperature and Lubricant Condition
Imbalance applies cyclic radial loading to bearings. Over time, that additional load can contribute to heat, lubricant distress, cage damage, and rolling-element fatigue, depending on bearing type, load, speed, lubrication, and contamination.
Temperature alone does not diagnose imbalance. Lubricant quantity, lubricant type, seal condition, preload, electrical damage, and process heat can all influence it.
Still, a rise in bearing temperature combined with increasing radial 1× vibration deserves attention. Treat the combination as a maintenance signal rather than waiting for a bearing defect frequency to dominate the spectrum.
🛢️ Understand the Cost to Bearings
Bearings are designed for loads, but unbalance adds a rotating load that repeatedly changes direction. The bearing does not experience one steady force; it experiences a cyclic demand each revolution.
This can reduce fatigue margin and increase shaft motion, particularly when the machine operates near a structural resonance or has limited support stiffness. In fluid-film bearings, excessive shaft orbit can also affect film behavior and clearances.
Correcting imbalance early is therefore a load-management action. It protects not only the bearing but also the housing, fit surfaces, seals, and lubricant system around it.
🤝 Understand the Cost to Couplings
Couplings transmit torque, but they also experience the consequences of rotor motion. Excessive vibration can accelerate wear in flexible elements, fretting at hubs, bolt loosening, and fatigue in associated hardware.
An imbalanced rotor does not automatically mean the coupling is defective. Conversely, a worn coupling can add clearance or instability that makes vibration analysis less straightforward.
When a coupling shows unusual wear, inspect alignment, rotor condition, support integrity, and operating transients together. Replacing only the flexible element may treat the symptom rather than the forcing source.
🧰 Use Portable Vibration Tools Wisely
A handheld vibration meter can be a valuable screening tool when used consistently. It can reveal that a machine has changed and help prioritize a more complete assessment.
A vibration analyzer with a tachometer reference provides more diagnostic power through spectra, phase, time waveform, and trend collection. For balancing work, reliable phase reference and repeatable sensor placement are particularly important.
Instrument quality does not eliminate the need for correct setup. Verify sensor mounting, speed input, frequency range, measurement units, and whether readings represent displacement, velocity, or acceleration.
📉 Read Overall Values in Context
Overall vibration values are useful for trending, but they combine energy from multiple frequencies. A rising overall value may result from imbalance, bearing damage, looseness, gearmesh activity, or another source.
Conversely, a meaningful increase in 1× vibration can be diluted in an overall reading if unrelated broadband vibration is already high. Use overall values for screening and spectral data for diagnosis when available.
Machine acceptance limits and alarm levels should come from applicable site practice, equipment requirements, and relevant standards where used. A universal number is not a substitute for knowing the machine’s duty and baseline.
🧮 When Field Balancing Is Appropriate
Field balancing is appropriate when evidence supports residual rotor imbalance and the machine is otherwise mechanically sound. It is especially useful when the assembled rotor cannot be practically balanced in a shop under its actual operating conditions.
A qualified practitioner identifies correction planes, collects baseline amplitude and phase, applies a secure trial weight if the procedure allows, and calculates permanent correction. Corrections may involve adding weight, removing material, or adjusting purpose-designed balance hardware.
The work requires a documented risk assessment. Never attach improvised weights to a running rotor, and never perform balancing where correction hardware cannot be reliably retained at maximum speed.
🏭 When Shop Balancing Is the Better Choice
Remove the rotor for shop balancing when it is damaged, heavily fouled, newly manufactured, repaired, or unsuitable for safe field correction. A balancing machine can assess the component under controlled conditions and may identify issues that are difficult to resolve in place.
Shop balancing does have limits. The installed machine can still vibrate because of fit-up, alignment, supports, aerodynamic loading, or resonance. A well-balanced rotor is necessary in many cases, but it is not proof that the installation is healthy.
For critical equipment, retain balance reports and component configuration details. Changing a hub, key arrangement, or attached accessory later may alter the result.
📝 A Practical Diagnostic Sequence
Use a disciplined sequence to avoid treating every 1× peak with weights:
- Confirm the reported symptom, operating speed, load, and recent maintenance history.
- Collect repeatable vibration data in radial and axial directions, ideally with a tachometer reference.
- Compare the spectrum and phase with baseline data or similar healthy equipment.
- Inspect supports, fasteners, soft foot, obvious rubbing, alignment condition, and coupling assembly.
- Check the rotor for deposits, erosion, damaged blades, missing hardware, or geometric runout.
- Assess whether resonance or process conditions are amplifying the response.
- Balance only after competing mechanical causes have been reasonably addressed.
- Verify the result at normal operating conditions and document the final readings.
This sequence is not a replacement for site procedures, but it prevents a common failure mode: making a balance correction to compensate for a fault that remains active.
🚫 Common Shortcuts That Create Worse Problems
Several shortcuts repeatedly lead to misleading conclusions or unsafe work:
- Balancing before checking for loose mounts, soft foot, or misalignment
- Using a single overall vibration value as proof of imbalance
- Comparing measurements taken at different locations or sensor orientations
- Ignoring process changes, speed changes, and thermal growth
- Adding correction mass without a calculated method or secure retention
- Assuming a newly replaced bearing means the root cause is gone
- Cleaning only the visible side of a fouled impeller or fan
The correction that appears quickest is not always the correction that lasts. Good diagnosis narrows uncertainty before any rotor modification is made.
🧑🏭 Build Imbalance Checks into Routine Maintenance
Routine routes should include more than a casual listening check. Record vibration trends, bearing temperatures, unusual noise, evidence of loose hardware, and changes in process performance.
After work that disturbs rotating parts—such as impeller cleaning, fan blade repair, coupling replacement, or motor changeout—schedule a verification run. Early post-maintenance measurements catch assembly errors before the machine returns to unattended service.
For process equipment prone to buildup, address the source as well as the symptom. Repeated balancing will not be efficient if the material adhesion, washdown practice, filtration issue, or operating condition remains unchanged.
🦺 Keep Safety at the Center of Testing
Rotating equipment can cause severe injury. Measurements near operating machinery require guards, safe access, secure cables, appropriate personal protective equipment, and compliance with site rules.
Inspections requiring contact with the rotor, coupling, or driven equipment must be completed under the applicable isolation and lockout procedure. Do not defeat interlocks or remove guards for convenience.
Field balancing should be assigned to personnel who understand the instrument, rotor construction, correction method, and hazards of retained weights. If the machine’s condition is uncertain, stop and escalate rather than experimenting at speed.
✅ The Core Principle: Find the Force Before Correcting It
Shaft imbalance is fundamentally a rotating force problem. Its common 1× signature, speed dependence, and radial vibration pattern make it detectable, but those clues must be interpreted alongside phase, machine condition, alignment, support stiffness, and process behavior.
The most reliable approach is to establish a baseline, investigate changes systematically, inspect the mechanical system, and use balancing only when the evidence supports it. That process protects bearings and couplings because it removes the actual source of cyclic loading rather than temporarily reducing a symptom.
Detecting imbalance early is less about reacting to a noisy machine and more about recognizing a repeatable vibration pattern, confirming its cause, and correcting it safely. ⚙️📈🛠️