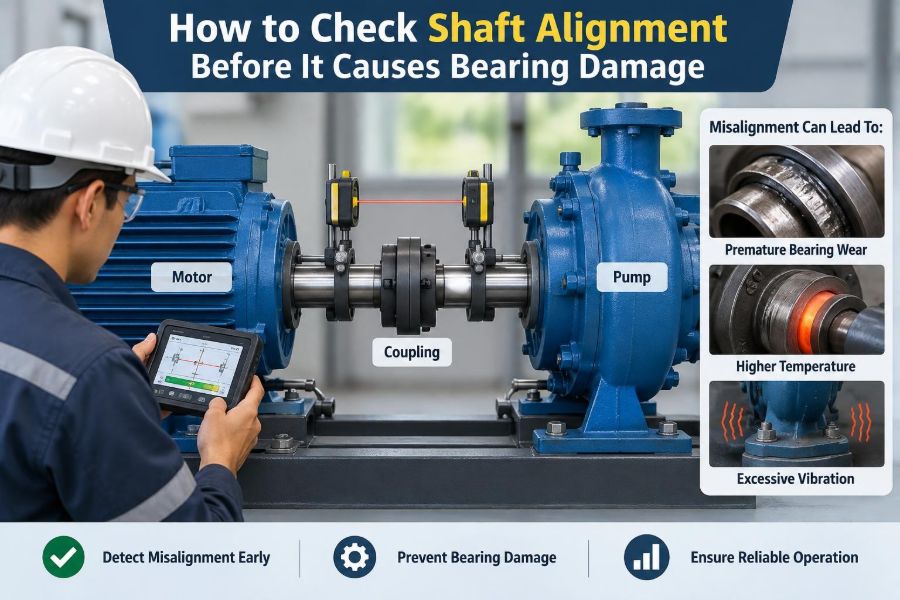

A pump and motor can sound normal during a quick walk-by, then begin consuming bearings, seals, and coupling elements far sooner than expected. The usual repair response is to replace the failed part. Yet the new bearing may inherit the same loading that damaged the old one.
Shaft misalignment is a quiet source of trouble in rotating equipment. It can raise vibration, heat bearings, stress couplings, and waste energy without producing an immediately obvious failure. In a busy plant, that makes it easy to overlook until downtime forces the issue.
Checking alignment is not simply a matter of placing a straightedge across two shafts. It means establishing a stable machine condition, understanding what the measurements represent, and correcting the machine in a sequence that does not introduce new errors.
Whether the equipment is a small workshop drive or a process-critical pump train, a disciplined alignment check gives maintenance teams a chance to remove a damaging force before it becomes an expensive failure.
🔩 What shaft alignment actually means
Shaft alignment describes the geometric relationship between the rotating centerlines of two coupled machines. In a typical motor-pump train, the motor shaft and pump shaft should rotate about centerlines that meet correctly at the coupling under operating conditions.
“Correctly” does not always mean perfectly collinear when the machine is cold and stopped. A machine may move as it reaches operating temperature. The target is the specified alignment condition that produces acceptable shaft positions while running.
🧭 The two fundamental kinds of misalignment
Parallel, or offset, misalignment occurs when shaft centerlines are parallel but displaced. Imagine two straight railroad tracks side by side: they point in the same direction but never meet.
Angular misalignment occurs when centerlines meet at an angle. One shaft is effectively pointed slightly up, down, left, or right relative to the other. Real machines often have a combination of angular and offset error in both the vertical and horizontal planes.
| Condition | What changes across the coupling | Typical correction |
|---|---|---|
| Vertical offset | One shaft centerline sits higher than the other | Add or remove calculated shims |
| Vertical angularity | Vertical gap differs from one coupling side to the other | Change front and rear machine feet differently |
| Horizontal offset | One machine is laterally displaced | Move the movable machine sideways |
| Horizontal angularity | Machines point toward different lateral directions | Move front and rear feet by different amounts |
🛞 Why bearings feel the consequences
Bearings are designed to carry defined radial and axial loads while allowing low-friction rotation. Misalignment creates additional forces that travel through the coupling and shafts into bearing housings. The bearing may then operate with loading that is not centered as intended.
The result can be elevated temperature, altered lubricant film behavior, cage distress, raceway damage, or shortened grease life. Bearing damage has multiple possible causes, so alignment should be assessed alongside lubrication, fit, contamination, electrical erosion, and balance rather than assumed to be the sole explanation.
🔗 The coupling is flexible, not a cure
Flexible couplings accommodate limited relative motion and help transmit torque. They do not make large alignment errors harmless. A coupling that is repeatedly flexed beyond its intended working range can impose cyclic forces on connected equipment.
Elastomeric elements may crack or compress excessively; grid, gear, and disc couplings can wear or fatigue in different ways. Always use the coupling manufacturer’s allowable limits as one input, but do not confuse a coupling survival limit with the alignment target needed for long machine life.
🌡️ Start with operating history
Before placing instruments on the machine, review the failure pattern. Repeated bearing changes on the same end of a motor or pump, coupling insert wear, seal leaks, rising vibration after startup, or unusually hot bearing housings can justify an alignment investigation.
Ask what changed before the symptoms appeared: a motor replacement, base repair, piping modification, process temperature change, or relocation of the equipment. This context helps distinguish a persistent installation problem from a new condition.
👀 Use visual clues, but do not stop there
A visual inspection can reveal obvious issues: a coupling hub sitting unusually close to one side, damaged guards, loose anchor bolts, accumulated dirt under feet, distorted shims, or pipe connections that appear to pull on a pump casing.
These observations are useful screening evidence, not a precision measurement. A machine can look straight to the eye and still have enough angularity or offset to create harmful forces at operating speed.
🛑 Make the equipment safe to inspect
Alignment work exposes people to heavy components, pinch points, stored energy, and potentially hot process equipment. Isolate electrical and process energy according to the site’s lockout, tagout, and permit procedures before removing guards or working around the coupling.
Verify that rotation cannot occur unexpectedly. Allow surfaces to cool where necessary, use suitable lifting methods for motors or components, and reinstall all guards before returning the machine to service. Site rules and equipment manuals take priority over any general procedure.
📐 Know which machine should move
In many motor-driven trains, the driven machine—such as a pump, compressor, or gearbox—is treated as the stationary machine, and the motor is the movable machine. This convention simplifies communication because corrections are made at the motor feet.
It is not universal. The machine selected to remain fixed should be the one constrained by piping, process connections, foundations, or train geometry. Decide this before measuring; moving both machines without a plan can make corrections difficult to track.
🧱 Verify the base before measuring
An alignment instrument only reports the relationship of the machines at the moment of measurement. It cannot compensate for a cracked foundation, loose pedestal, deteriorated grout, or baseplate that bends when bolts are tightened.
Inspect bolt condition, base corrosion, and visible movement. If the support structure is unstable, precision alignment may not hold. Correct structural defects first, then align on a clean, sound, repeatable mounting condition.
🪨 Find soft foot before making alignment corrections
Soft foot exists when one or more machine feet do not sit flat on the base. Tightening the hold-down bolts bends the machine frame, changing the shaft position and potentially distorting bearing housings.
Check it by loosening one foot at a time while observing movement with an appropriate indicator or alignment system, following the instrument procedure. A meaningful lift or shift indicates that the foot condition must be corrected before final alignment values can be trusted.
🧰 Correct soft foot thoughtfully
Causes include dirt under a foot, burrs, damaged shims, uneven base surfaces, bent feet, and excessive or poorly fitted shim packs. Clean contact surfaces first. Replace corroded, folded, or too-small shims with clean, full-size shims appropriate to the foot.
Do not solve a serious soft-foot condition by forcing bolts tighter. Where a foot is distorted or the base is uneven, machining, base repair, or engineered shimming may be necessary. Recheck every foot after each correction because the condition can interact across the machine.
📏 Choose a measurement method that fits the job
A straightedge and feeler gauges can identify gross coupling misalignment on simple, low-speed equipment. They are inexpensive and useful for a preliminary check, but their accuracy and repeatability are limited by access, coupling geometry, and operator technique.
Rim-and-face dial indicators, reverse-dial methods, and laser alignment systems provide more complete information. The best choice depends on equipment criticality, coupling type, access, required tolerance, team skill, and whether records are needed for repeat maintenance.
🔍 Straightedge checks: useful for screening
Place a precision straightedge across accessible coupling hub rims at several clock positions. Gaps can indicate offset. Feeler gauges inserted between coupling faces at several positions can reveal angular differences.
This method is vulnerable to hub runout, imperfect surfaces, and difficulty reading small gaps. Use it to spot a clearly poor setup or for rough pre-alignment, not as a substitute for a controlled precision method where bearing life and reliability matter.
🕰️ Dial indicators and what they measure
Dial indicators convert small mechanical movement into a readable displacement. In a rim-and-face setup, one indicator observes radial movement at the rim while another observes axial movement at the coupling face as shafts are rotated together.
Readings must be interpreted with the machine geometry: coupling diameter, distance from coupling to feet, and indicator positions. Because the calculation can be sensitive to setup errors, document dimensions carefully and follow a recognized procedure for the selected method.
🛰️ Laser alignment systems reduce calculation burden
Laser systems use mounted sensors and a laser beam to determine relative shaft position through rotation. Many systems guide the user through measurement positions and calculate required foot moves, displaying vertical and horizontal corrections directly.
They improve repeatability and reduce arithmetic mistakes, but they are not automatic truth machines. Loose brackets, dirty mounting surfaces, shaft runout, inadequate rotation, incorrect dimensions, or a moving base can still produce misleading results.
🔄 Compensate for runout and measurement error
Coupling hubs and shafts are not perfectly round or concentric. As a hub rotates, runout can make an indicator or laser sensor report movement that comes from the surface itself rather than shaft centerline misalignment.
Rotate both shafts together where the method requires it, and use the instrument’s specified runout compensation or repeatability check. If readings change substantially between repeated setups, investigate the setup rather than averaging away an unexplained inconsistency.
↕️ Correct vertical alignment with controlled shimming
Vertical corrections are made by adding or removing shims under the movable machine feet. The required change is usually different at the front and rear feet when angularity is present, which is why calculated corrections matter.
Use clean stainless steel shims of suitable size and minimize the number in each stack. After changing shims, tighten bolts according to the equipment procedure and measure again. A loose-bolt reading does not represent the final operating support condition.
↔️ Correct horizontal alignment without forcing the machine
Horizontal moves are commonly made with jacking bolts, controlled side screws, or purpose-built positioning devices. Measure movement while adjusting, and avoid striking a machine with a hammer unless the equipment procedure specifically permits a carefully controlled method.
Forcing a motor sideways against piping, conduit, or an obstructed base can store stress that later releases. Ensure cables, guards, and ancillary connections have sufficient freedom before making the move.
🧮 Read alignment tolerances in context
Acceptable alignment depends on speed, coupling design, shaft spacing, bearing type, machine stiffness, and expected thermal movement. A tolerance suitable for a slow utility drive may be inappropriate for a high-speed process machine.
Use the equipment manufacturer’s requirements, coupling guidance, and the site reliability standard where available. Treat generic tolerance charts as orientation only. The meaningful question is whether the final condition is acceptable for this machine at its real operating state.
🔥 Account for thermal growth
Machine casings, shafts, supports, and piping expand as temperatures rise. If a hot pump grows upward more than its motor, an alignment that is perfect while cold can become vertically offset in service.
Thermal growth targets may be based on manufacturer data, operating measurements, or an established reliability program. They should not be guessed from a single temperature reading. Where uncertainty is high, trend operating vibration and repeat alignment checks after collecting better thermal information.
🧪 Consider process forces and pipe strain
Pipe strain occurs when connected piping pushes, pulls, or twists a machine casing. It may change shaft alignment as flanges are tightened or as the process reaches pressure and temperature. A pump can appear aligned with piping disconnected, then move after reconnection.
Check for movement while loosening or tightening connections only under an approved, safe procedure. Correcting pipe support, routing, flange fit-up, or expansion accommodation is preferable to using the machine casing as a structural member of the piping system.
📳 Use vibration as evidence, not a verdict
Misalignment can contribute to vibration patterns at running speed and its harmonics, particularly in the axial direction for some configurations. However, vibration signatures overlap with looseness, imbalance, bent shafts, resonance, gear issues, and hydraulic or aerodynamic effects.
Vibration data is valuable for deciding where to investigate and for confirming whether a correction improved behavior. It does not replace physical alignment measurement, and alignment results do not eliminate the need to investigate other vibration causes.
🌡️ Watch temperature, lubrication, and seals
Higher bearing housing temperature, degraded grease, leaking seals, and coupling heat can support the case for investigating alignment. These symptoms are not unique: excessive lubricant, wrong lubricant, contamination, seal installation problems, or process conditions can produce similar observations.
Record baseline conditions before adjustment when practical. Comparing temperature, vibration, and visual condition before and after a verified alignment correction provides a more useful maintenance record than relying on memory.
🧷 Tighten bolts and recheck the final condition
Alignment can shift when hold-down bolts are tightened, especially on flexible bases or where soft foot remains. Tighten in the specified sequence and torque range, then perform a final measurement with the machine fully secured.
Also check that jacking bolts are backed off or locked as required, shims remain seated, and no tool or temporary support is influencing the frame. Final readings should be recorded after the machine has reached its installed condition.
📝 Record more than the final numbers
A useful alignment record includes the machine identification, date, operating condition, selected stationary machine, method used, dimensions, initial readings, soft-foot observations, shim changes, horizontal moves, final readings, and any thermal targets.
Note unusual factors such as pipe strain, base damage, coupling condition, or restricted machine movement. These details let the next technician understand why a value was accepted and make recurring movement easier to identify.
⚠️ Common practices that undermine good alignment
- Aligning before correcting soft foot: bolt tightening changes the result.
- Using old, damaged shim packs: the machine may not be supported uniformly.
- Ignoring thermal movement: a good cold reading may not be good while running.
- Trusting one measurement pass: repeatability matters.
- Moving the wrong machine by habit: process connections and train constraints may be disturbed.
- Stopping at coupling tolerance: the coupling may survive while bearings remain unnecessarily loaded.
🏭 A practical sequence for a motor-pump train
- Review symptoms, operating changes, and applicable alignment targets.
- Isolate the equipment and inspect the coupling, base, bolts, shims, and piping.
- Select the stationary and movable machines.
- Check and correct soft foot on the movable machine.
- Mount the selected alignment tools securely and compensate for runout as required.
- Measure the initial vertical and horizontal condition.
- Make vertical shim corrections first, then horizontal moves.
- Tighten, remeasure, document, reinstall guards, and verify behavior after startup.
This sequence may need adjustment for turbines, multi-element trains, vertical pumps, or equipment with special manufacturer instructions. The principle remains: stabilize first, measure carefully, correct deliberately, and verify after assembly.
🧩 Special cases require extra judgment
Spacer couplings, long shaft spans, cardan shafts, vertical machinery, and trains with three or more machines introduce geometry that is not captured by a simple two-machine routine. Some machines must be aligned to deliberately offset targets or evaluated at several operating states.
For high-energy, high-speed, or safety-critical equipment, involve qualified personnel and use the machine manufacturer’s procedures. Precision tools improve the work, but competence in interpreting the machine system remains essential.
📅 Build alignment into preventive maintenance
Alignment is most effective when it is part of a reliability routine rather than an emergency response. Check it after installation, motor replacement, major coupling work, base or piping modifications, and repeated vibration or bearing issues.
A periodic check can also be reasonable for machines known to experience thermal cycling, foundation settlement, or frequent process changes. The interval should reflect equipment criticality and observed stability, not a one-size-fits-all calendar rule.
🎯 The core principle: align the whole machine system
Good shaft alignment is not achieved by chasing a display until it turns green. It depends on stable feet, a sound base, reliable measurements, appropriate targets, secure fasteners, and an understanding of how heat and connected piping affect the machine.
When these conditions are addressed together, alignment removes a preventable source of load from bearings, seals, shafts, and couplings. It is a practical example of precision maintenance: small geometric corrections can protect the performance of an entire rotating system.
Check the machine’s support and operating conditions before trusting its alignment numbers, then verify the result after every correction. That disciplined approach helps bearing replacements become less frequent repairs and more reliable assets. ⚙️🔧📈